CUSTOM MANUFACTURING & TOOLING
Manual Vs Cryogenic Silicone Deflashing: Manual Deflashing vs Cryogenic Deflashing for Silicone Parts: Which Route Fits?
Compare manual and cryogenic silicone deflashing by geometry, edge quality, process control, volume, total cost and B2B approval evidence.
DIRECT ANSWER
What B2B Buyers Need to Know
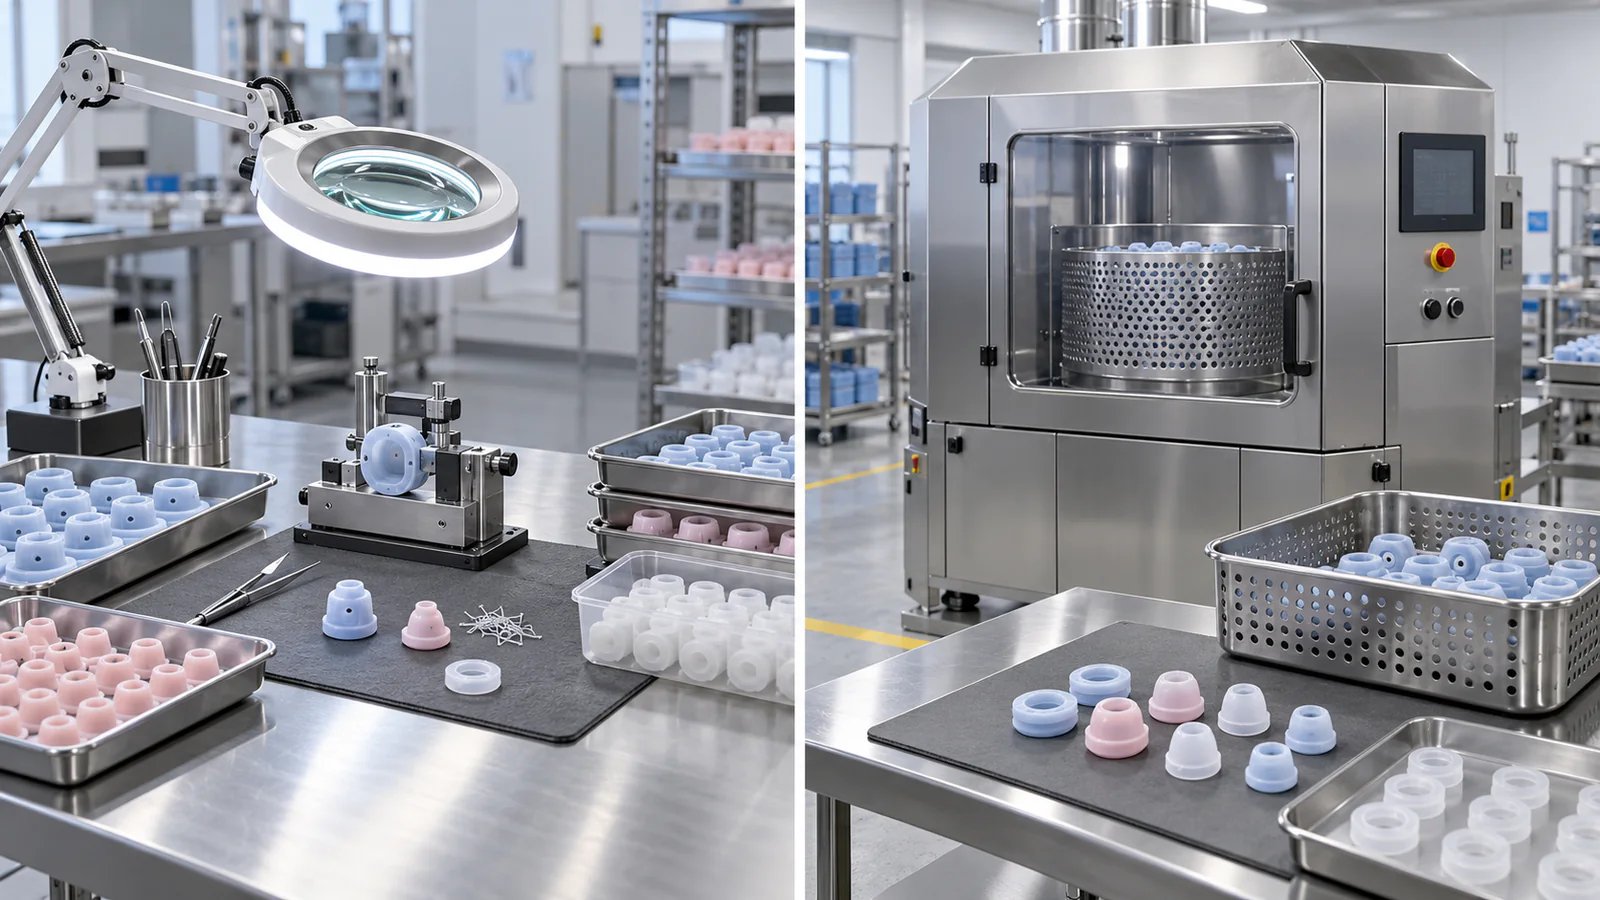
Manual deflashing usually fits complex, low-volume or protected silicone geometries that need selective operator control. Cryogenic deflashing can fit repeatable higher-volume parts whose thin flash separates within a validated cooling, agitation and media window. Buyers should approve neither route by name alone; compare production-representative samples, edge zones, damage risk, yield, total cost, capacity and traceability.
This guide is written for silicone product engineers, sourcing managers, quality teams, tooling buyers, contract manufacturers and private-label product owners. It provides a decision framework rather than legal advice or a universal specification. Product classification, use conditions and destination market should be confirmed before final testing, labelling or compliance decisions.
Key Takeaways
- Define flash, trim witness, loose-particle and damage limits by product zone before choosing a route.
- Use manual deflashing for selective access only when fixtures, tools, training and variation are controlled.
- Use cryogenic deflashing only inside a validated load, cooling, agitation, media and cleaning window.
- Compare both routes with the same molding lot, critical zones, conditioning and acceptance evidence.
- Model total cost from yield, rework, inspection, batch size, capacity and lead-time risk—not unit price alone.
- Treat recurring heavy flash as a molding or tooling escalation, not unlimited secondary-process work.
Manual vs Cryogenic Silicone Deflashing Decision Matrix
Use this matrix to structure supplier trials. Final route, performance, price, minimum quantity, capacity and timing remain conditional on the actual part and approved process window.
| Decision factor | Manual deflashing | Cryogenic deflashing |
|---|---|---|
| Geometry | Selective access around complex, large, fragile or protected zones | Best evaluated on robust parts with accessible thin flash and suitable batch handling |
| Primary control | Fixture, tool, operator sequence, blade condition and visual standard | Equipment, load, temperature profile, time, agitation, media and cleaning |
| Typical risk | Nicks, overcut, uneven witness, fatigue and operator-to-operator variation | Residual flash, media, whitening, impact marks or thin-feature damage |
| Volume behavior | Flexible for low or mixed runs but direct labor grows with output | Can support repeatable larger batches but adds setup, queue and minimum-load effects |
| Evidence | Timed pilot by operator or shift plus edge, dimensional and functional results | Repeated cycles across representative loads plus residue, edge and recovery results |
| Commercial model | Labor, fixtures, supervision, inspection, rework and staffing risk | Equipment, cryogen, media, batch utilization, screening, cleaning and yield |
SECTION 01
Define the Finished Edge and Candidate Parts
Convert the commercial concept into controlled dimensions, functions and approval criteria before DFM begins.
Define the Flash and Finished-Edge Requirement for manual vs cryogenic silicone deflashing
Start with the finished edge, not the name of the secondary process. Flash can appear at a mold parting line, insert shutoff, vent, overflow, or gate area, and each location can have a different consequence for sealing, assembly, appearance, cleaning, or user handling. A buyer therefore needs a zoned drawing that distinguishes critical edges from ordinary cosmetic boundaries.
For each zone, define the allowed flash, step, tear, trim witness, and loose-particle condition using measurable limits or approved boundary samples. ISO 3302-1 provides useful dimensional-tolerance and flash-classification context for molded rubber products, but it does not choose manual or cryogenic deflashing and it does not approve a particular finished silicone edge.
Photographs alone are weak acceptance standards because lighting, magnification, and angle change what inspectors see. We prefer a drawing linked to identified acceptable, limit, and reject samples, plus the viewing distance and magnification used at inspection. That package gives the factory, buyer, and third-party inspector the same definition before quotation or trial production begins.
Map Geometry, Part Size and Material Behavior
Part geometry determines whether a route can reach the flash without damaging the functional body. Manual trimming can follow a local contour, support a thin lip in a fixture, and protect a visible face, while cryogenic equipment treats a batch through controlled cooling, agitation, and media impact. Neither description proves suitability until the actual part and flash geometry are tested.
Record overall size, section transitions, undercuts, slots, sealing beads, hinges, membranes, texture, and any metal or plastic insert. Very soft compounds, thin flexible features, sharp external corners, and large parts may respond differently from compact robust shapes even when the nominal hardness matches. Mixed-color or multi-material parts also require separate residue and surface reviews.
Material behavior must be tied to the approved compound and cure condition. ISO 37 can provide a controlled method for comparing tensile stress-strain properties of rubber specimens, but a tensile report cannot predict finished-edge quality after either deflashing route. Production-representative parts still need route-specific trials after the molding process and post-cure, if used, are stabilized.
Understand Manual Deflashing Control and Labor
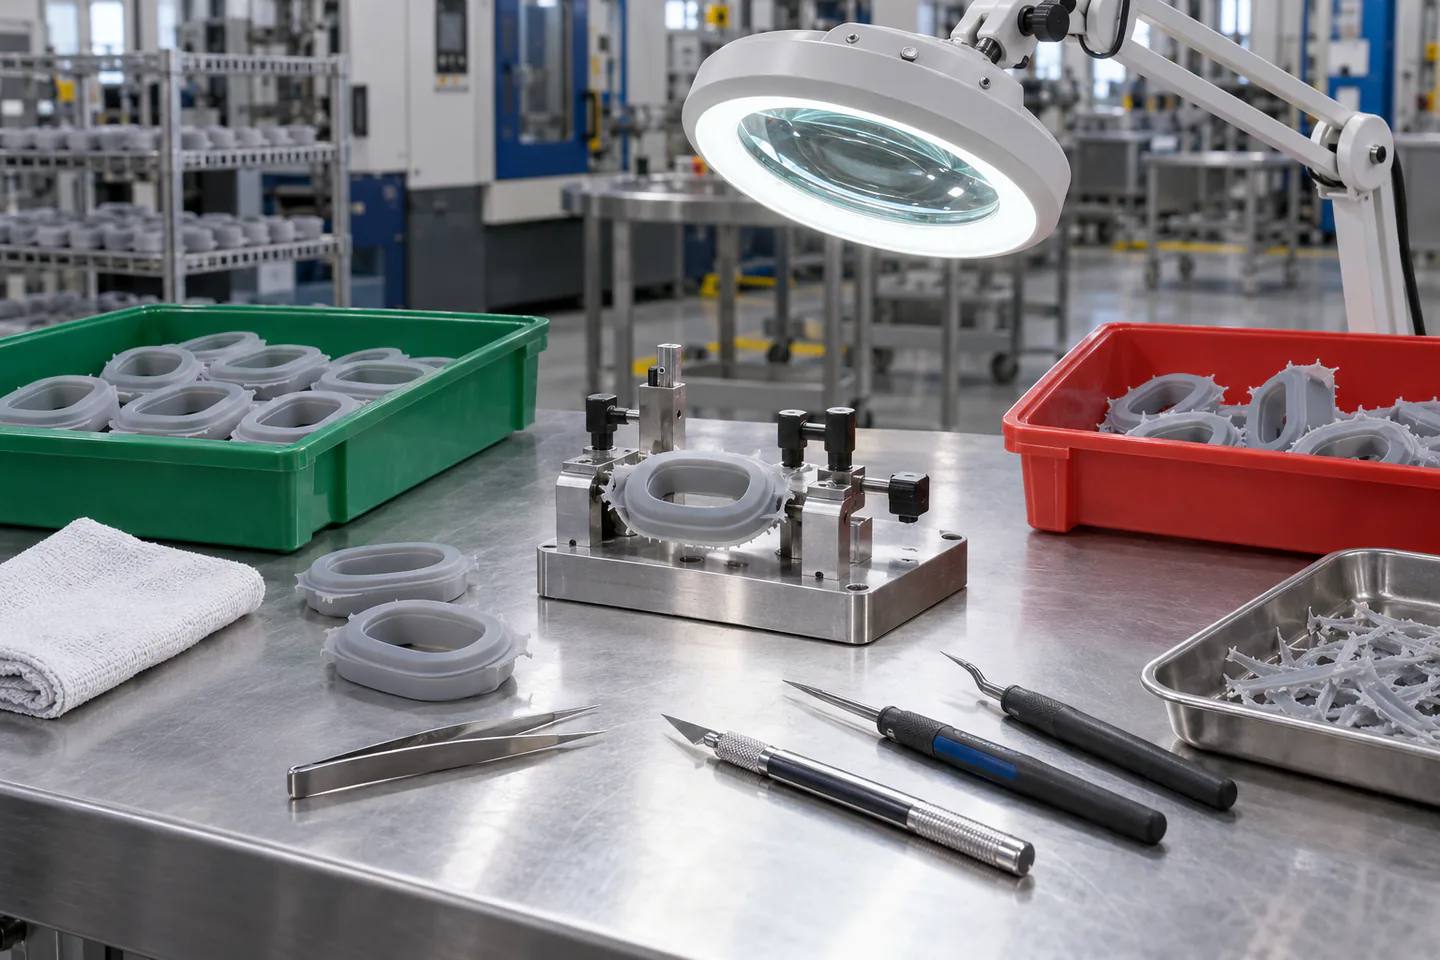
Manual deflashing is a controlled hand operation performed with knives, scissors, rotary tools, fixtures, magnification, or purpose-built gauges. Its strength is selective access: an operator can support a delicate section, change tool angle around a corner, and leave a specified witness at a critical interface. That flexibility is useful for complex parts, mixed low-volume orders, and early engineering changes.
The main risk is variation between people, shifts, tools, and fatigue levels. A work instruction should define the fixture, blade or tool type, sequence, safe hand position, maximum passes, prohibited contact zones, and inspection frequency. Training records and approved samples matter because a general instruction to trim cleanly cannot establish repeatable output.
Manual work also creates capacity and lead-time exposure when volume rises. The quotation should state expected pieces per labor hour, staffing assumption, inspection burden, rework allowance, and changeover time without presenting those estimates as guaranteed production rates. We confirm them during a timed pilot using the real part, tools, packaging orientation, and acceptance standard.
SECTION 02
Compare Manual and Cryogenic Process Control
Close the process, material and mold decisions that determine tooling scope, trial evidence and revision cost.
Understand Cryogenic Deflashing Equipment and Media
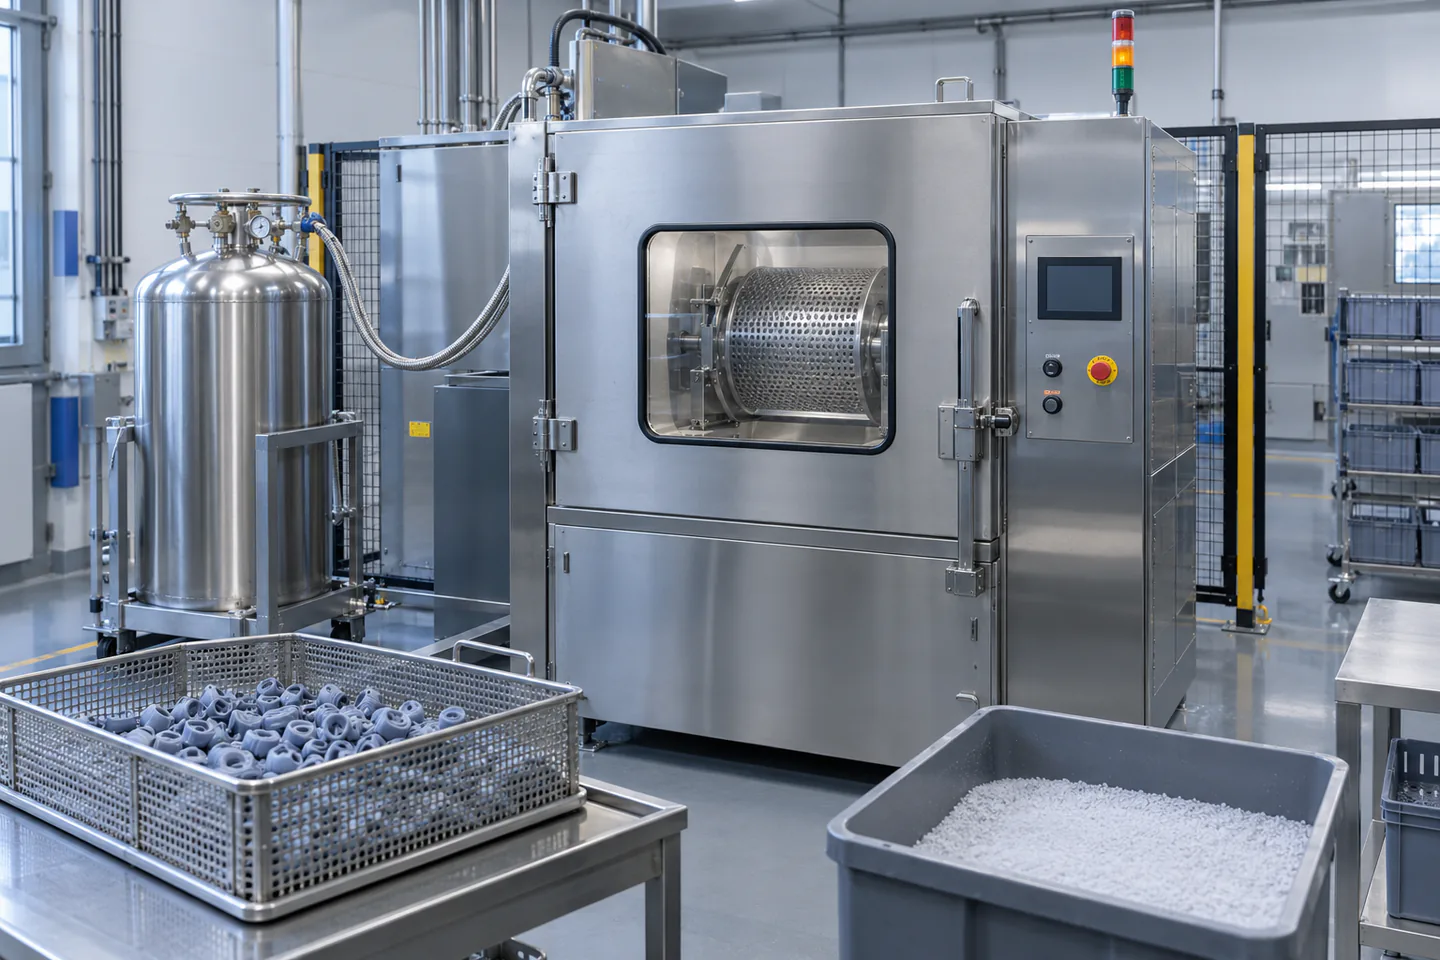
Cryogenic deflashing cools molded elastomer flash so it becomes easier to break away while the functional part remains sufficiently resistant within a controlled process window. Parts are processed in guarded equipment with a defined load, temperature profile, exposure time, rotation or agitation, and selected media. The route can be attractive for repeatable high-volume batches with accessible thin flash.
The machine name is not a process specification. A supplier should record equipment identity, basket or chamber loading, part orientation, media material and size, cycle settings, screening, warming, and cleaning steps. Each parameter can change flash removal, surface marks, trapped media, dimensional recovery, or the probability of damage to thin features.
Safety and environmental controls belong to the factory process, including guarded equipment, ventilation, cryogen handling, maintenance, and trained operators. Buyers do not need proprietary machine settings in every case, but they should receive enough controlled evidence to know that the approved cycle is repeatable and that an unapproved recipe change cannot silently reach production.
Compare Edge Damage, Residue and Dimensional Risk
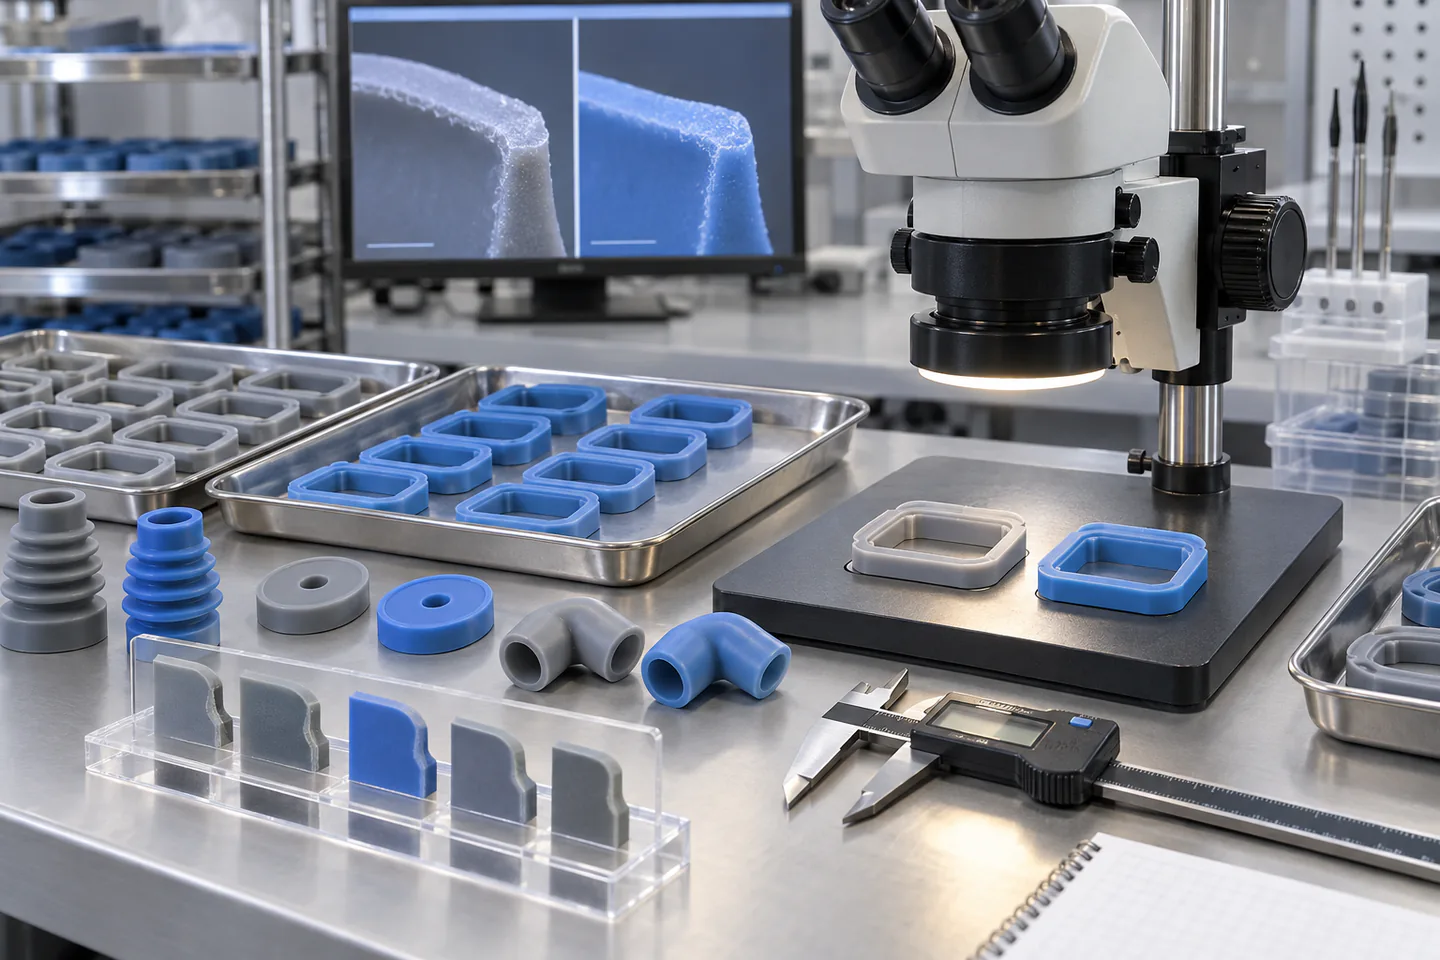
Finished-edge risk is broader than whether visible flash remains. Manual trimming may create a nick, gouge, uneven witness, or local overcut, while cryogenic processing may leave residual flash, media contamination, whitening, impact marks, or damage to unsupported features. The inspection plan must look for the characteristic failure modes of the selected route.
Critical sealing beads, food-contact edges, skin-contact boundaries, and snap or assembly interfaces deserve separate acceptance zones. Inspectors should check the edge under agreed lighting and magnification, then verify any dimension or function that can change after trimming. Loose fragments are assessed independently from attached flash because they create a different contamination and handling risk.
Dimensional checks should use agreed conditioning and datums after the part returns to a stable state. A compliant molded dimension before finishing does not prove that the finished component still seals or assembles, and a visually clean edge does not prove dimensional conformity. Route approval requires appearance, measurement, and functional evidence considered together.
Build Route-Specific Trial and Acceptance Criteria
Run a designed comparison trial instead of asking both suppliers for their best-looking samples. Use the same compound, mold revision, molding lot, cure status, and flash condition, then divide identified parts between manual and cryogenic routes. Retain unprocessed controls so the team can distinguish molding variation from finishing effects.
The trial plan should specify sample quantity, route parameters, critical zones, measurement method, visual limits, functional tests, cleaning, and packaging. Record pass, rework, and reject results by cavity where possible, because a cavity with heavy or misplaced flash can make one finishing route appear unstable when the underlying mold condition is the real cause.
Approve the process window, not one presentation sample. Repeat the selected route across representative loads, operators or cycles, and review edge quality after the intended post-finish handling. If a borderline result changes with load size, media age, blade condition, or inspector judgment, resolve that sensitivity before it becomes a shipment-level dispute.
SECTION 03
Validate Quality, Volume and Total Cost
Treat each mold trial as a measured engineering gate rather than a visual sample-selection exercise.
Match Process Choice to Volume and SKU Mix
Volume and SKU mix often decide the commercial route after technical feasibility is established. Manual deflashing can avoid equipment-specific setup and handle frequent geometry changes, while cryogenic processing can reduce direct touch time when parts, flash, batch size, and demand are suitable. The crossover point is project-specific rather than a universal annual-volume number.
Compare equivalent cost elements: labor, fixtures, equipment allocation, cryogen and media, screening, cleaning, inspection, rework, scrap, changeovers, maintenance, and work-in-process. A low unit finishing price can hide a high reject risk or a large minimum batch, while a higher manual rate may be rational for mixed short runs that would otherwise wait for a machine campaign.
Forecast by SKU, color, revision, and release date. A program with many small call-offs may not behave like one large order even if annual volume is identical. Ask the supplier to state the assumed batch size, utilization, shift pattern, queue, and material availability behind quoted capacity and lead time, then keep those commercial figures conditional until the production plan is approved.
Control Lot Identity, Rework and Mixed Output
Lot identity must survive the secondary operation. Trays, baskets, work orders, and temporary containers should identify part number, revision, color, compound lot, molding lot, cavity range, finishing route, and status. This control becomes especially important when accepted parts, parts awaiting finishing, and rework share the same production area.
Define what rework is allowed and how many cycles or manual interventions a part may receive. Repeating a cryogenic cycle or trimming an already damaged edge can change the risk profile, so rework should follow an approved instruction and remain traceable. Parts outside that instruction should be segregated rather than blended back into conforming output.
After finishing, use a controlled cleaning and count-reconciliation step appropriate to the product. Media, trimmed fragments, and mixed parts must not travel into final packaging. The batch record should reconcile issued, accepted, reworked, rejected, sampled, and retained quantities so a yield improvement is supported by evidence instead of being created by an accounting gap.
Compare Tooling Correction Against Secondary Finishing
Secondary finishing should not become a permanent substitute for a correctable mold problem. Heavy, irregular, or rapidly changing flash can indicate wear, poor shutoff, vent condition, clamp or process instability, or damage. Engineering should compare the recurring cost and risk of trimming with the corrective cost of restoring the tool or process.
Create escalation triggers for flash width, location, rework rate, operator time, cryogenic residue, and edge defects. When a trigger is exceeded, quarantine the affected lot and review molding data before increasing finishing intensity. More aggressive trimming may temporarily improve appearance while increasing nicks, scrap, or cycle exposure.
A tooling correction must be revalidated because moving a parting line or changing a shutoff can alter dimensions, texture, venting, and the approved witness. Keep before-and-after samples and update the drawing, visual standard, process route, and inspection plan together. This closes the loop between mold maintenance and secondary finishing instead of managing them as unrelated departments.
SECTION 04
Release the Route and Control Repeat Orders
Release production only when drawings, golden samples, inspection records and change authority describe the same revision.
Model Total Cost, Capacity and Lead-Time Risk
Total cost includes the consequences of variation, not only the quoted finishing charge. Model expected yield, rework, inspection, scrap, delay, complaint handling, and inventory exposure for each route. Use ranges when rates are not yet proven, and identify which pilot result or production record will replace each assumption.
Capacity claims should describe the approved part and process window. Machine availability does not equal qualified capacity if baskets, media, cleaning, inspection, or trained people are constrained, and a large manual team does not guarantee consistent output without fixtures and supervision. Ask for the bottleneck, planned utilization, and backup response for the order scenario.
Lead time should separate molding, conditioning or post-cure, finishing queue, inspection, packing, and shipment release. A supplier may recommend a hybrid plan in which cryogenic processing removes accessible flash and controlled manual work handles protected zones, but that combination requires its own route, costing, trials, and traceability rather than inheriting approval from either process alone.
Release the Process and Control Repeat Orders
Production release starts with a signed package: drawing and flash zones, approved compound and color, mold revision, route and process window, boundary samples, functional tests, inspection method, packaging, and change-control rules. Supplier and buyer should identify which records accompany each shipment and which are retained for trend review or complaint investigation.
Use in-process checks to detect drift before final inspection. Blade condition, operator confirmation, cycle parameters, load count, media status, and first-off edge results can be recorded at frequencies based on risk. Final lot inspection may use an agreed sampling plan such as an ISO 2859-1 framework, but shipment sampling does not replace process validation or checks of critical characteristics.
For repeat orders, compare yield, defect location, rework, and cycle or labor data against the approved baseline. Require written review before compound, mold, cavity, equipment, media, fixture, tool, work instruction, inspection method, or production site changes. A stable deflashing route is one that remains connected to the exact product evidence the buyer approved.
ACTION FRAMEWORK
Buyer Checklist Before Commercial Approval
Use this checklist as a meeting agenda. It is intentionally concise so the team can identify missing evidence without replacing its own quality, legal or supplier-management procedure.
| Check | Question | Why It Matters |
|---|---|---|
| Edge zones | Are sealing, assembly, appearance and ordinary edges classified separately? | One flash limit can hide very different functional consequences. |
| Part baseline | Are compound, cure, mold revision, cavity and molding lot controlled? | Finishing comparisons are invalid when incoming flash conditions differ. |
| Manual route | Are fixture, tools, sequence, training and inspection frequency documented? | Operator skill alone cannot establish repeatable production control. |
| Cryogenic route | Are load, cycle, agitation, media, cleaning and equipment identity controlled? | The machine name does not define the approved process window. |
| Damage review | Are nicks, residue, whitening, impact and loose fragments assessed? | Removing visible flash can introduce a different unacceptable defect. |
| Route trial | Were both routes compared on identified production-representative parts? | Presentation samples may not represent cavity, batch or load variation. |
| Total cost | Do quotations include yield, rework, inspection, batch size and queue assumptions? | A finishing unit price alone cannot predict landed manufacturing cost. |
| Change control | Must compound, mold, equipment, media, fixture and work-instruction changes be approved? | Any of these changes can invalidate the finished-edge evidence. |
NEXT READING
Continue the Supplier and Product Review
These internal resources connect the guide with Naike Silicone product, factory, customization and inquiry pages. Open the route that matches the next decision in your project.
Review silicone compression mold design decisions
Use review silicone compression mold design decisions to gather the next level of product, manufacturing or commercial information.
Open internal resource →Compare single- and multi-cavity silicone molds
Use compare single- and multi-cavity silicone molds to gather the next level of product, manufacturing or commercial information.
Open internal resource →Build a silicone tooling approval plan
Use build a silicone tooling approval plan to gather the next level of product, manufacturing or commercial information.
Open internal resource →Review Naike Silicone quality-control capabilities
Use review naike silicone quality-control capabilities to gather the next level of product, manufacturing or commercial information.
Open internal resource →Explore all silicone product categories
Use explore all silicone product categories to gather the next level of product, manufacturing or commercial information.
Open internal resource →Review Naike Silicone manufacturing knowledge
Use review naike silicone manufacturing knowledge to gather the next level of product, manufacturing or commercial information.
Open internal resource →PRIMARY REFERENCES
Authoritative External Sources
The sources below are official primary references. Applicability depends on the product, intended use and destination market. Buyers should obtain qualified advice for final legal or regulatory decisions.
ISO 3302-1:2014 Rubber Product Dimensional Tolerances
Official ISO page for dimensional tolerance classes and flash-classification context for solid molded rubber products; it does not select a finishing route or approve a product-specific silicone edge.
ISO 37:2024 Rubber Tensile Stress-Strain Properties
Official ISO page for the method used to determine tensile stress-strain properties of vulcanized and thermoplastic rubbers; finished-lid fit still requires product-specific validation.
ISO 2859-1:2026 AQL Sampling for Lot-by-Lot Inspection
Official ISO page for the current sampling schemes indexed by acceptance quality limit for lot-by-lot inspection by attributes.
BUYER QUESTIONS
Frequently Asked Questions
Is cryogenic deflashing always faster than manual trimming?
No. Cryogenic equipment can reduce direct touch time for suitable high-volume parts, but loading, cooling, media, screening, cleaning, inspection, minimum batch size and queue time still matter. Compare both routes using the same part, acceptance standard and order scenario. The faster commercial route can change with geometry, batch size, SKU mix and proven yield.
Which silicone parts are better candidates for manual deflashing?
Manual work is often useful for complex contours, protected functional zones, large parts, thin unsupported features, mixed short runs and designs still changing during development. Suitability depends on fixture access, operator control and measurable edge limits. A timed pilot should confirm repeatability, capacity and damage risk before the route is released.
Can very soft silicone parts be cryogenically deflashed?
Possibly, but nominal hardness is not enough to approve the route. Compound formulation, section thickness, feature support, cure condition, flash geometry, temperature profile, agitation and media all influence the result. Test production-representative parts across the proposed process window and inspect recovery, surface condition, dimensions, loose residue and functional zones.
What samples should a buyer request during process comparison?
Request identified unprocessed controls, manual-route samples and cryogenic-route samples from the same molding lot, preferably with cavity traceability. Include normal and challenging geometries, acceptable and limit samples, dimensional results, functional checks, route parameters, yield and defect records. Review the samples after normal cleaning, conditioning and packaging rather than only at the machine.
How should flash and trim quality be written on a drawing?
Divide the part into functional and cosmetic zones, then define allowed attached flash, step, trim witness, loose particles, nicks and gouges for each zone. State the datum, measurement or visual method, lighting, magnification and boundary samples. Do not rely on terms such as clean edge or no flash without a measurable or physical reference.
What should a B2B RFQ include for silicone deflashing?
Provide the 3D data and drawing, compound and hardness, mold and cavity information, expected flash condition, annual and batch volumes, SKU mix, critical edge zones, visual and dimensional limits, functional tests, cleaning and packaging requirements. Ask suppliers to quote route assumptions, trial plan, yield, rework, capacity, lead time, change control and the cost of tooling correction where relevant.
Editorial and Scope Note
Conclusion: Manual vs Cryogenic Silicone Deflashing
Move from buyer research to a controlled supplier brief
Select manual, cryogenic or a controlled hybrid deflashing route only after the same production-representative silicone parts pass zoned edge, dimensional, functional, cleanliness and packaging checks. Send Naike Silicone your drawing, compound, mold status, batch forecast, critical zones and acceptance limits to request a route comparison, tooling review, trial samples and conditional quotation.
This factory-insider guide supports sourcing preparation and supplier discussion; it does not replace product-specific engineering, laboratory, regulatory, legal or commercial review for the destination market.